 EN
Quick Links
Industrial equipment operating in mining, quarrying, cement, steel, power generation, and bulk material handling environments is often exposed to severe wear. Hard and abrasive materials can continuously impact, slide, or flow across equipment surfaces, gradually removing the underlying metal and reducing component service life.
A hardfacing liner plate provides a dedicated wear-resistant surface designed to protect equipment from these demanding conditions. Unlike conventional steel liners, hardfacing liner plates combine a structural substrate with a wear-resistant overlay, allowing the surface to withstand severe abrasive conditions while the base material provides mechanical support.
However, selecting the right hardfacing liner plate requires more than choosing the highest hardness or thickest overlay. The correct specification depends on the material being handled, dominant wear mechanism, impact intensity, operating temperature, equipment geometry, and required service life.
This guide explains the key factors industrial buyers and engineers should consider when selecting a hardfacing liner plate for maximum wear protection.
A hardfacing liner plate is a composite wear-resistant component consisting of a base plate and a hardfacing layer.
The base plate provides structural support, while the hardfacing layer is designed to resist surface wear.
The overlay can contain hard phases such as chromium carbides distributed within a metallic matrix. These hard structures help resist the cutting, scratching, and grinding action of abrasive particles.
Hardfacing liner plates are commonly used to protect:
Chutes
Hoppers
Conveyors
Crusher components
Feed systems
Bins
Transfer points
Mining equipment
Material handling systems
The liner acts as a replaceable wear surface, protecting the more expensive equipment structure underneath.
Conventional structural steel can provide excellent mechanical strength but may wear rapidly when exposed to highly abrasive materials.
Replacing an entire chute, hopper, or machine component because of surface wear can result in:
High material costs
Long maintenance periods
Production downtime
Increased labor requirements
Unplanned equipment repairs
A hardfacing liner plate provides a sacrificial wear surface.
Instead of allowing the equipment structure to absorb the full abrasive load, the liner takes the majority of the wear.
This approach can extend equipment service intervals and make maintenance more predictable.
The first step in selecting a hardfacing liner plate is identifying how the equipment actually wears.
Sliding abrasion occurs when abrasive material continuously moves across the liner surface.
Typical applications include:
Chute bottoms
Hopper walls
Conveyor liners
Material transfer surfaces
For these applications, high surface wear resistance is usually a primary consideration.
Impact occurs when large or heavy particles strike the liner surface.
It is common around:
Crusher feed areas
Rock boxes
Loading zones
Dump hoppers
Transfer points
Impact-heavy applications require consideration of both the hardfacing layer and the toughness of the substrate.
Fine particles moving at high velocity can gradually remove material from the liner.
This type of wear can occur in high-speed material handling or pneumatic conveying systems.
Many industrial applications experience multiple wear mechanisms simultaneously.
For example, material may initially impact a liner and then slide across its surface.
In these cases, the liner must provide a balanced combination of abrasion resistance and mechanical performance.
The material passing over the liner has a major influence on wear rate.
Before selecting the liner, determine:
Material type
Hardness
Particle size
Particle shape
Density
Moisture
Temperature
Abrasiveness
Hard, angular particles generally produce more aggressive abrasive action than soft or rounded particles.
For mineral processing applications, information about the ore composition and particle distribution can also help improve liner selection.
Particle size affects both abrasion and impact.
Large particles can create substantial impact forces, particularly when falling from a significant height.
Fine particles may produce continuous sliding or erosive wear.
Provide the manufacturer with:
Average particle size
Maximum particle size
Minimum particle size
Particle size distribution
This information helps determine whether the application requires greater impact resistance, abrasion resistance, or a combination of both.
Material velocity can significantly influence liner wear.
As particles move faster, the energy and frequency of contact with the liner can increase.
Important parameters include:
Conveyor speed
Chute flow velocity
Material discharge velocity
Feed rate
Maximum operating speed
High velocity can be especially important in transfer systems and areas where the material changes direction.
A hardfacing liner plate should therefore be selected based on actual flow conditions rather than the equipment name alone.
Impact severity depends on several factors.
These include:
Drop height
Particle size
Particle density
Material velocity
Impact angle
Throughput
A liner installed beneath a large rock drop point may experience substantially greater impact than one installed along a downstream sliding surface.
This is why liner thickness and material specifications may need to vary between different sections of the same equipment.
Hardfacing liner plates can be manufactured using different overlay compositions and technologies.
One common solution for severe abrasive applications is a chromium carbide-rich hardfacing layer.
The hard carbide phases provide strong resistance to abrasive material removal.
Other material systems may be appropriate depending on:
Abrasion severity
Impact
Temperature
Corrosion
Material characteristics
Required service life
The best material should be selected according to the dominant failure mechanism rather than simply choosing the highest nominal hardness.
Overlay hardness is an important indicator of abrasion resistance.
A harder surface can provide strong resistance against many abrasive materials.
However, hardness should not be evaluated independently.
If an application involves substantial impact, the relationship between:
Hardness + Toughness + Microstructure + Substrate Support
becomes particularly important.
An extremely hard surface may not provide the best overall solution if the operating environment generates severe mechanical shock.
For chromium carbide hardfacing systems, the carbide structure can have a significant influence on wear performance.
Important characteristics may include:
Carbide distribution
Carbide morphology
Matrix structure
Carbide concentration
Overlay uniformity
A consistent microstructure can contribute to predictable wear behavior.
For demanding industrial applications, buyers should consider whether the manufacturer has appropriate quality-control and metallographic inspection capabilities.
Overlay thickness determines the available wear allowance.
As abrasive material gradually removes the surface, the hardfacing layer becomes thinner.
The required thickness depends on:
Expected wear rate
Abrasiveness
Impact intensity
Target service life
Equipment clearance
Installation conditions
An excessively thick liner may increase weight and cost without providing proportional benefits.
The optimal thickness should be based on expected material loss during the planned service interval.
The base plate is an important part of the complete liner system.
It provides support for the hardfacing layer and contributes to:
Structural strength
Toughness
Fabrication
Installation
Resistance to mechanical loading
For applications with high impact, substrate selection becomes particularly important.
The hardfacing layer and substrate should work together rather than being evaluated as separate materials.
Hardfacing liner plates can be used on different equipment surfaces, including:
Flat surfaces
Curved sections
Hopper walls
Chute transitions
Conveyor components
Deflector plates
The liner should fit the equipment geometry accurately.
Poor fitting can create gaps, unsupported areas, or material accumulation, potentially accelerating localized wear.
For complex equipment, customized dimensions and prefabricated components may reduce installation work.
Wear is rarely uniform across an entire machine.
Typical high-wear areas include:
Material impact points
Chute inlets
Hopper outlets
Transfer points
Direction changes
Crusher feed zones
Conveyor loading areas
These locations may require:
Increased liner thickness
Higher wear resistance
Different liner profiles
Additional reinforcement
Instead of using one specification everywhere, engineers can develop a zone-based protection strategy.
Some industrial applications operate at elevated temperatures.
Examples include:
Cement production
Steel processing
Slag handling
High-temperature material transfer
Temperature can affect the performance of the substrate, overlay, and joining system.
Before selecting a hardfacing liner plate, determine:
Normal operating temperature
Maximum temperature
Duration of exposure
Temperature fluctuations
The material should be suitable for the complete thermal environment.
Abrasion is not always the only source of material degradation.
Wet or chemically active environments can produce combined abrasion and corrosion.
Relevant factors include:
Moisture
Slurry chemistry
pH
Chemical additives
Chloride exposure
Operating temperature
If corrosion contributes significantly to component failure, the liner system should be evaluated for both mechanisms.
Hardfacing liner plates may need to be fabricated before installation.
Typical operations include:
Cutting
Drilling
Welding
Grinding
Forming
Edge preparation
The hardfacing layer contains hard phases that can make fabrication more demanding than conventional steel.
Fabrication procedures should therefore be established before production.
For large projects, factory-prefabricated liner sections can reduce cutting and fitting work at the installation site.
Many hardfacing liners are installed by welding them to the equipment structure.
The welding process should account for:
Substrate properties
Overlay characteristics
Heat input
Preheating requirements
Welding consumables
Heat-affected zones
Improper welding procedures can create unnecessary thermal stress or affect the integrity of the liner system.
Installation instructions should be provided according to the specific liner construction.
Liner thickness and material density affect overall component weight.
This matters when installing large liner sections because heavier components can increase:
Lifting requirements
Installation time
Labor requirements
Structural loading
The liner should provide sufficient wear allowance without creating unnecessary weight.
A hardfacing liner should be selected according to a defined service-life target.
Service life can be measured by:
Operating hours
Tons processed
Production cycles
Maintenance intervals
For critical equipment, the target service life should ideally align with planned maintenance schedules.
Historical wear data can help establish realistic expectations.
Initial purchase price should not be the only procurement criterion.
A better evaluation includes:
Purchase cost + fabrication + installation + maintenance + replacement + downtime
A higher-performance liner may cost more initially but provide:
Longer operating periods
Fewer replacements
Lower maintenance labor
Reduced equipment downtime
Better production continuity
For high-throughput industrial operations, these factors can have a significant effect on total operating cost.
The manufacturer's production capability can influence liner performance and consistency.
When evaluating a supplier, consider:
Hardfacing technology
Overlay control
Production capacity
Quality management
Material testing
Dimensional inspection
Microstructure control
Custom fabrication
Technical support
For repeated procurement, batch consistency is particularly important.
Consistent overlay thickness, hardness, dimensions, and material properties make maintenance planning more predictable.
Before requesting a quotation, prepare detailed operating information.
| Selection Factor | Information to Provide |
|---|---|
| Equipment type | Chute, hopper, conveyor, etc. |
| Material handled | Ore, coal, rock, slag, etc. |
| Particle size | Average and maximum |
| Particle hardness | Available data |
| Material velocity | Normal and maximum |
| Throughput | Tons per hour |
| Wear mechanism | Sliding, impact, erosion, etc. |
| Impact conditions | Drop height and impact angle |
| Temperature | Normal and maximum |
| Corrosion | Chemical and moisture conditions |
| Liner dimensions | Length, width, thickness |
| Overlay thickness | Required or target |
| Substrate | Required base material |
| Installation | Welding, bolting, etc. |
| Service life | Hours or tons processed |
Providing this information enables the manufacturer to recommend a more application-specific liner configuration.
Hardness does not fully determine liner performance. Toughness, microstructure, substrate properties, and overlay thickness also matter.
A liner designed primarily for sliding abrasion may not be suitable for severe impact conditions.
More material does not always mean better economics. Excessive thickness can increase weight and installation costs.
Poorly fitted liners can create unsupported areas and localized wear.
High-impact and high-abrasion zones may require different protection levels.
The lowest purchase price may not result in the lowest cost over the equipment's operating life.
Cutting, welding, lifting, and fitting requirements should be considered during procurement rather than after delivery.
Selecting the right liner is only the first step.
Reducing unnecessary impact and turbulence can help lower localized wear.
Additional wear protection can be concentrated where material contact is most severe.
Regular measurements can reveal actual wear rates and help predict replacement requirements.
Correct fitting and welding help ensure that the liner performs as designed.
Previous liner performance can provide valuable information for improving future specifications.
A liner should be replaced before excessive wear reaches the underlying equipment structure.
Customized liner plates can be useful when standard products do not match the equipment or operating conditions.
Customization may include:
Non-standard dimensions
Special overlay thickness
Custom shapes
Prefabricated sections
Reinforced impact areas
Different wear specifications for different zones
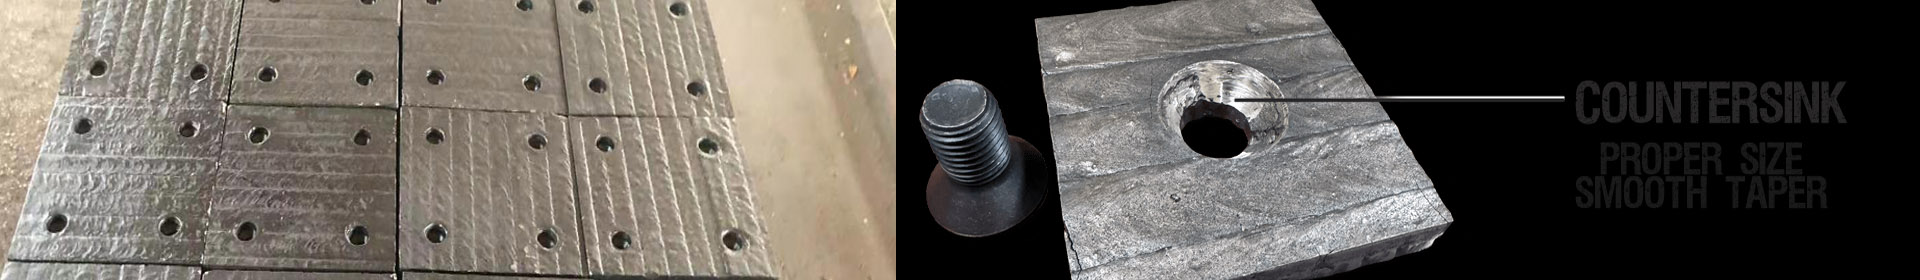
Customized mounting holes
Special edge preparation
Customized solutions can reduce field fabrication and help place wear protection precisely where it is required.
Selecting the right hardfacing liner plate for maximum wear protection requires a complete understanding of the operating environment.
The most important considerations include:
Material characteristics
Wear mechanism
Particle size
Material velocity
Impact intensity
Overlay hardness
Carbide structure
Overlay thickness
Substrate properties
Equipment geometry
Temperature
Corrosion
Installation requirements
Required service life
Lifecycle cost
A high-quality hardfacing liner plate is not simply a harder piece of steel. Its performance depends on the interaction between the wear-resistant overlay, substrate, manufacturing process, and actual operating conditions.
For severe abrasive applications, chromium carbide-based hardfacing can provide a highly wear-resistant surface capable of protecting critical equipment components from continuous material loss.
By matching liner material, overlay thickness, substrate properties, and liner configuration to the specific wear environment, industrial operators can improve equipment protection, extend maintenance intervals, reduce replacement frequency, and achieve more predictable long-term operating costs.
Copyright © Shenyang Hard Welding Surface Engineering Co., ltd. - Privacy policy